Manufacturing
Manufacturing
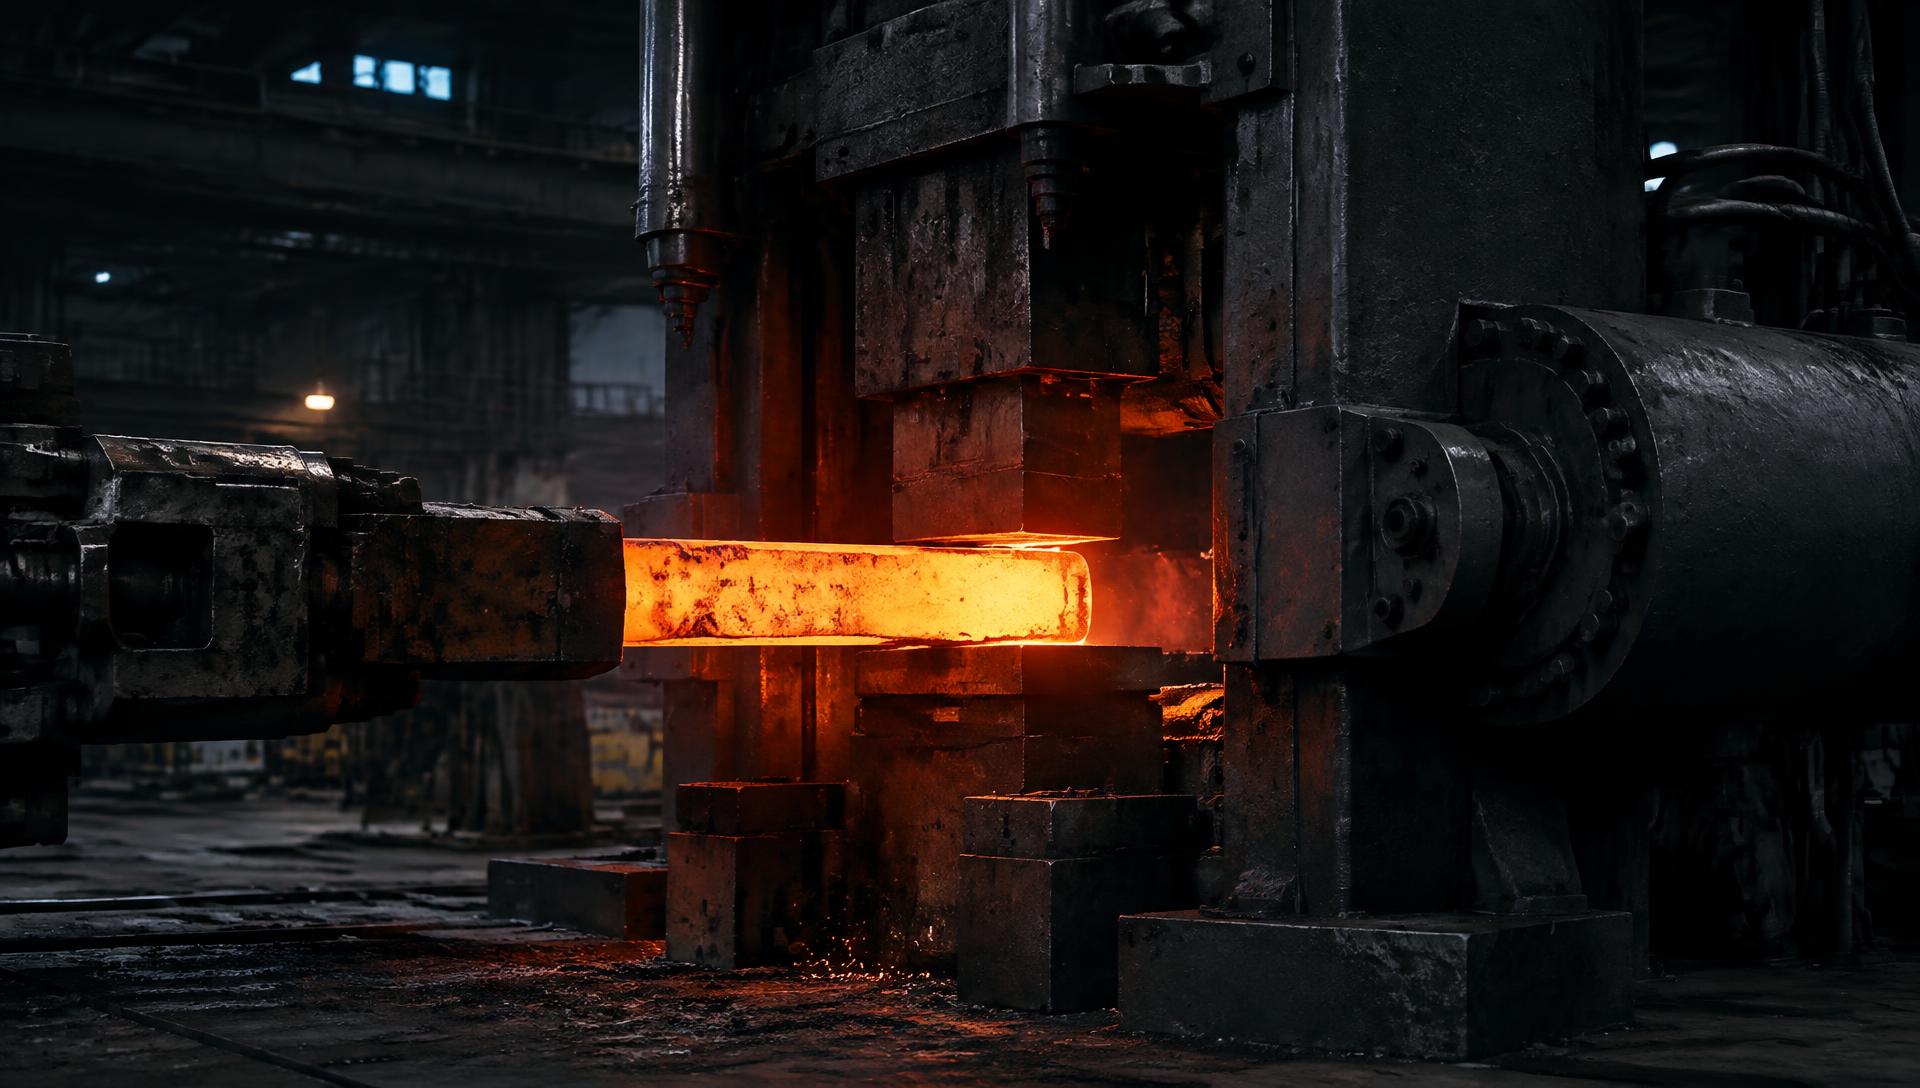
The tool room and the forge work on one site, so the die and the part take shape in the same place.
Plant figures
- Annual output
- 7.500t / year
- Part weight
- 200 g – 60 kg
- Covered area
- 7.000m² covered
- Plant site
- 55.000m² site
Process
Hot forging flow
- 01
Material
Steel is cut to length according to the weight and section of the part to be made.
- 02
Heating
The cut steel is heated up to the temperature at which forging can be done.
- 03
Forging
The hot steel is pressed inside a die made in the tool room and moves toward the part shape.
- 04
Trimming and sizing
Flash and excess material are removed so the part approaches its dimension.
- 05
Preparation and dispatch
The part is identified, packed and made ready for domestic or export shipment.
The steps below describe a general hot forging flow. Press tonnage and heating equipment are not published as plant data.
Technical processes
From design to flash control
 01
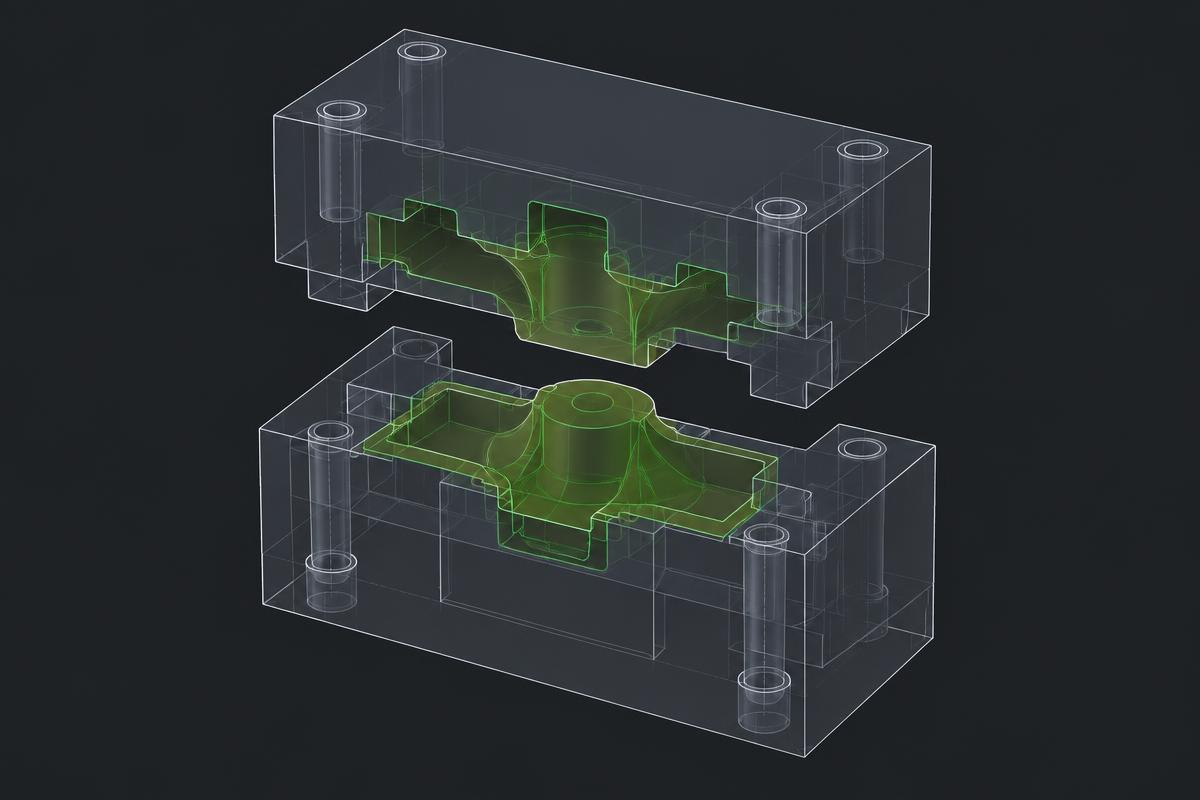
3D die design
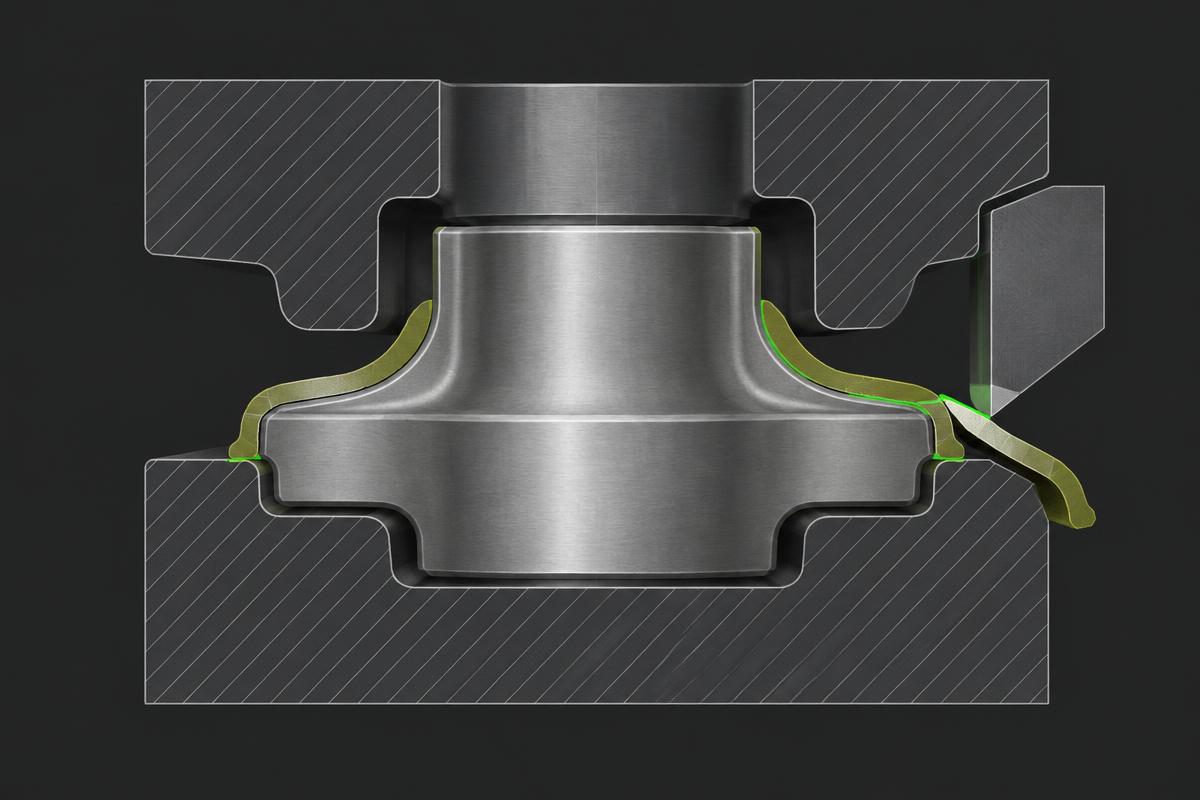
The part geometry is modelled in three dimensions; die cavities, the filling sequence and the flash land geometry are decided at this stage.
 02
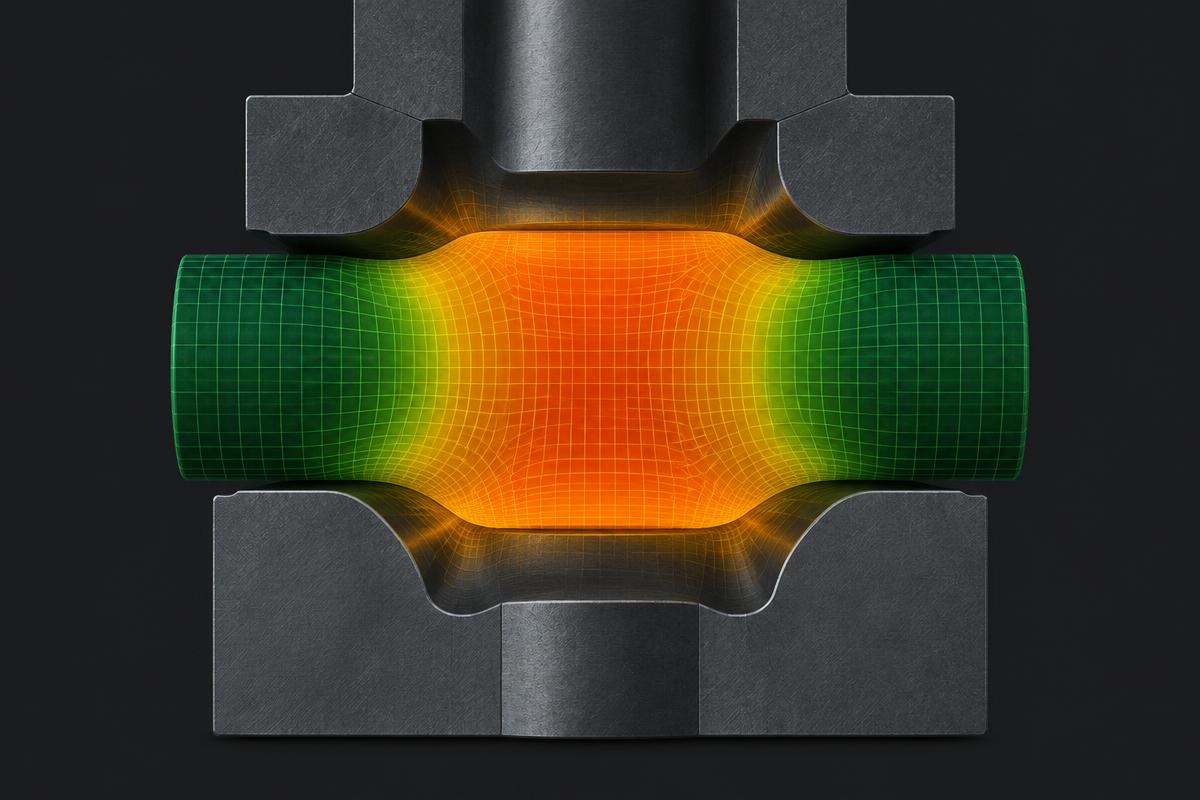
Forging simulation
Before steel is cut, the material flow is simulated; risks such as folding, underfill and excess flash become visible in the die, reducing the number of trials.
 03
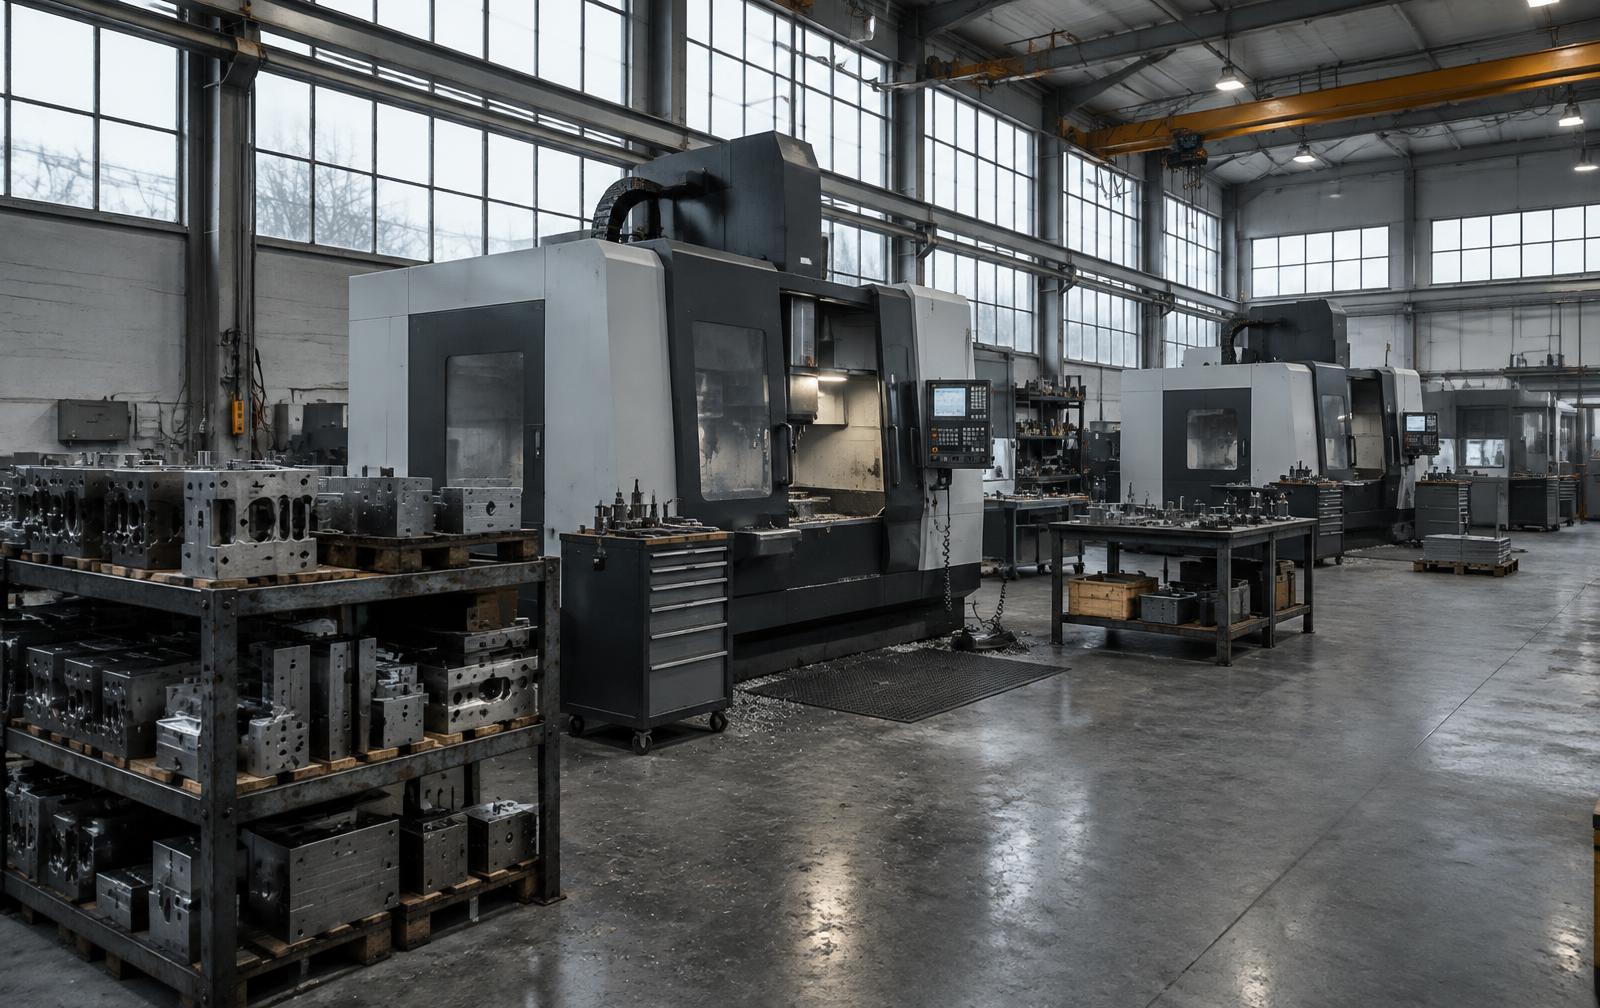
Die making and trials
The die is opened on the same site according to the approved model; a first trial part is produced and revised until its dimensions are confirmed.
 04
Flash control
After forging, the flash is trimmed; section and dimensional checks bring the part to the allowances fixed at the design stage.
These stages are carried out in our own die shop; no die is opened before the design and simulation outputs are settled.
Die shop
The die shop under the same roof as the forge
The die shop was set up as part of the 1989 investment and dies are opened on the same site. Corrections between the first die trial and series production are made in house.