Products
Gears and gear blanks
Forged gears and gear blanks in different modules and diameters.
Forging Simulation
How this part is forged
Explore billet heating, preforming, finishing dies and trimming stages.
Temperatures show the typical hot-forging range for steel (approx. 1,100–1,250 °C) as general engineering values, not plant measurements. Actual values depend on steel grade and part.
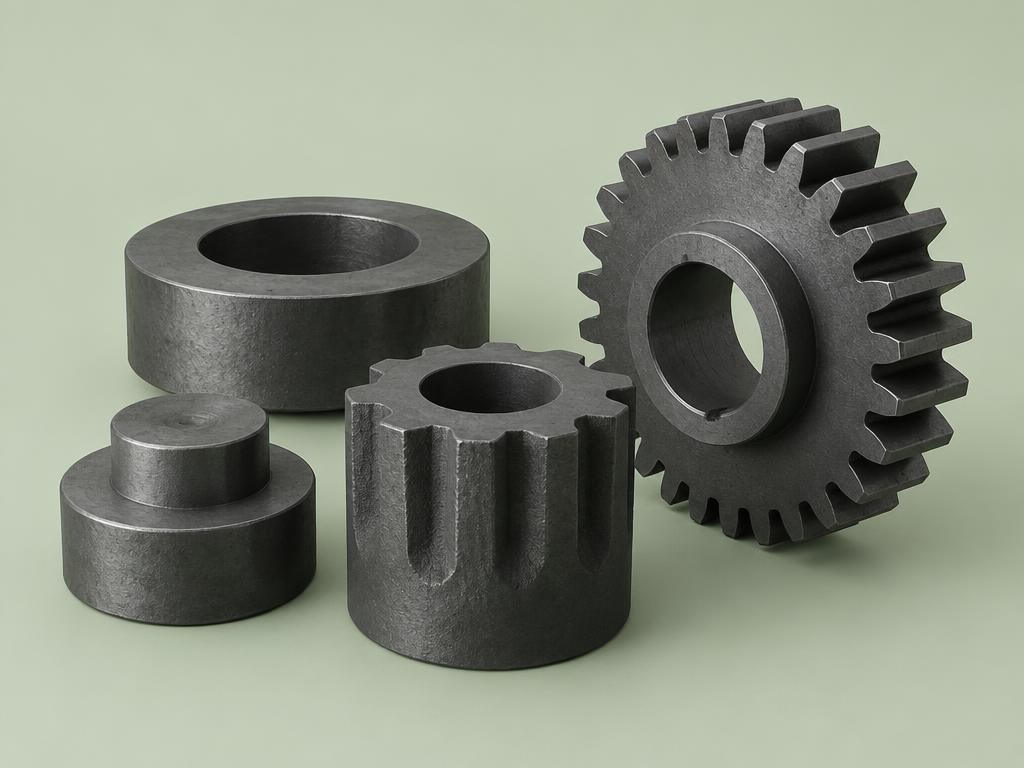
Forged gears and gear blanks are used in gearboxes, differentials and power-transmission units. The blank provides the base shape before gear cutting and heat treatment.
Forging orients the grain flow around the tooth area, supporting root strength. Blanks in various diameters and thicknesses are produced close to shape to reduce chip loss.
Parts listed in this group
2 parts- Gears
- Gear blanks
These are the part names the plant ships under. Weight, section and material set a separate die and forging plan for each part.
One die per part
A dedicated die and forging plan for each part.
To drawing
Made from a drawing or a sample.
Domestic and export
Regular shipments to eight countries.
Process
How these parts are made
- 01
Material
Steel is cut to length according to the weight and section of the part to be made.
- 02
Heating
The cut steel is heated up to the temperature at which forging can be done.
- 03
Forging
The hot steel is pressed inside a die made in the tool room and moves toward the part shape.
- 04
Trimming and sizing
Flash and excess material are removed so the part approaches its dimension.
- 05
Preparation and dispatch
The part is identified, packed and made ready for domestic or export shipment.
Quotation
What we need for a quote
Drawing or sample
Technical drawing (PDF/STEP) or a physical sample.
Material
Steel grade or operating condition.
Quantity and weight
Annual requirement and approximate part weight.
Other product groups
Ask about a part in this group
We work from a drawing or a sample. Weight, material and annual requirement are enough.